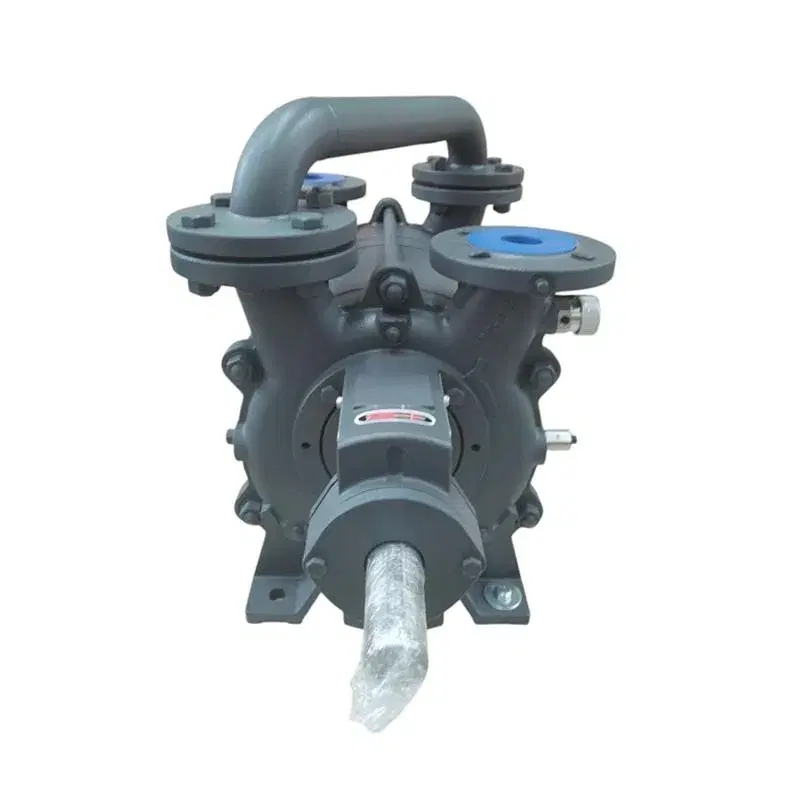
Double-Stage Liquid Ring Vacuum Pump
Two-stage liquid ring pump with 35–40% higher efficiency in high vacuum and lower energy use than single-stage designs.
- Max Capacity
- 110 – 1,717 m³/h
- Ultimate Vacuum
- 33 mbar
- Motor Power
- 3 – 75 kW
- Efficiency
- +35 – 40% in high vacuum
Highlights
- Genuine equipment supplied with warranty
- Professional installation & commissioning
- 24/7 after-sales support nationwide
- Genuine spare parts stocked locally
The DLV series is a double-stage liquid ring vacuum pump that holds a steady suction speed deep into high vacuum, or maintains high vacuum across a wide range of suction speeds. Compared with single-stage pumps it delivers 35–40% higher efficiency in high vacuum while consuming 15–20% less energy across the 25–1013 mbar range. Material options (carbon steel, stainless, duplex, titanium), single or double mechanical seals and imported bearings suit demanding food, pharmaceutical, chemical, power, paper, textile and metallurgy duty. Suction capacity runs from 110 to 2,600 m³/h.
You May Also Need
Related Products
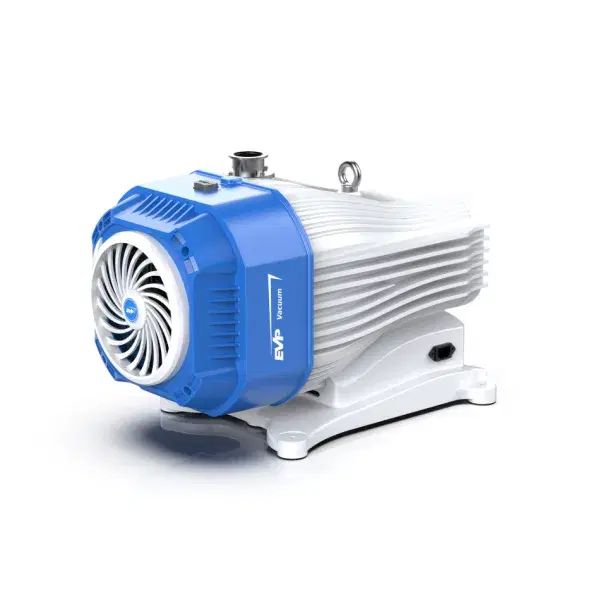
Dry Scroll Vacuum Pump
Completely oil-free and water-free scroll vacuum pump for clean applications such as labs, semiconductors and medical equipment.
View details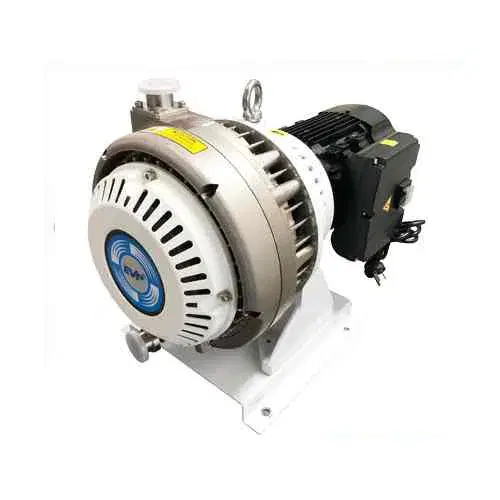
Dry Scroll Vacuum Pump (16 – 60 m³/h)
Higher-capacity oil-free scroll vacuum pump for clean industrial and laboratory vacuum from 4.4 to 16.6 L/s.
View details
Dry Screw Vacuum Pump
Oil-free dry screw vacuum pump that handles condensable vapours and solids without residue for chemical and process duty.
View details
Boxed Dry Screw Vacuum Pump
Enclosed, mobile-framed dry screw vacuum pump with side-panel connections and optional PLC/WiFi monitoring.
View details